Map the adhesive location
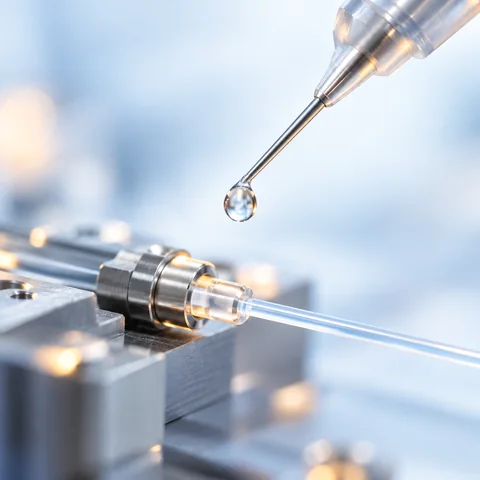
Define whether the material is in or near the optical path, the bond-line dimensions and the surfaces that must remain free of contamination.
Match flow to the assembly process
Viscosity and wetting should suit dispensing access, gap filling, capillary movement and the time available for active or passive alignment.
Control cure and alignment movement
Record UV access, irradiance or dose, fixture strategy, cure sequence and any shadowed area; evaluate movement during and after cure on the actual assembly.
Balance rigidity, shrinkage and stress
The required support, flexibility and thermal behavior depend on the substrate combination and alignment tolerance.
Qualify optical stability
Measure insertion loss or other relevant optical outputs before and after the intended thermal, moisture and mechanical reliability sequence.
INFORMATION CHECKLIST
Prepare these details for a productive material discussion.
- Optical path and adhesive location
- Substrates and bond-line geometry
- Dispensing and alignment sequence
- UV access and cure strategy
- Optical and environmental reliability tests
TECHNICAL FAQ
Questions to clarify before evaluation
Is the lowest-shrinkage adhesive always the best choice?
No. Flow, cure access, rigidity, stress management and the complete reliability requirement also affect selection.
Why should cure movement be measured on the actual assembly?
Substrate, bond-line and fixture conditions influence alignment response and cannot be represented by one bulk material value.
Which information should be shared for product selection?
Share the optical path, substrates, geometry, dispensing and alignment process, cure access and reliability tests.